Industrial EMC is no longer a box-checking exercise. In a factory, a variable-frequency drive can disturb a nearby sensor, while a long cable can turn a small interference problem into an intermittent line stoppage. The best Industrial EMC Solution in 2026 must therefore fit the equipment, installation, and operating environment—not just a laboratory test.
The scale of industrial automation makes this practical. The International Federation of Robotics’ World Robotics 2024 report counted 4.28 million industrial robots operating worldwide in 2023, up 10 percent from the previous year. More robots mean more controllers, drives, sensors, and communication links sharing crowded electrical environments. That creates more opportunities for conducted and radiated interference. It does not mean every plant needs the same fix.
A dependable selection starts with evidence. IEC 61000-6-2 and IEC 61000-6-4 provide immunity and emissions requirements for many industrial environments, but the correct standards depend on the product and installation. Check the test configuration, cable lengths, grounding method, and operating loads; small setup differences matter. Look for documented test results, suitable filters and shielding, and support that can investigate faults on site. Be cautious of broad claims such as “EMC-proof.” No solution can promise zero interference in every installation. That is an awkward truth, but an important one. In 2026, the strongest choice is the one that performs reliably under realistic conditions and can be verified after installation.
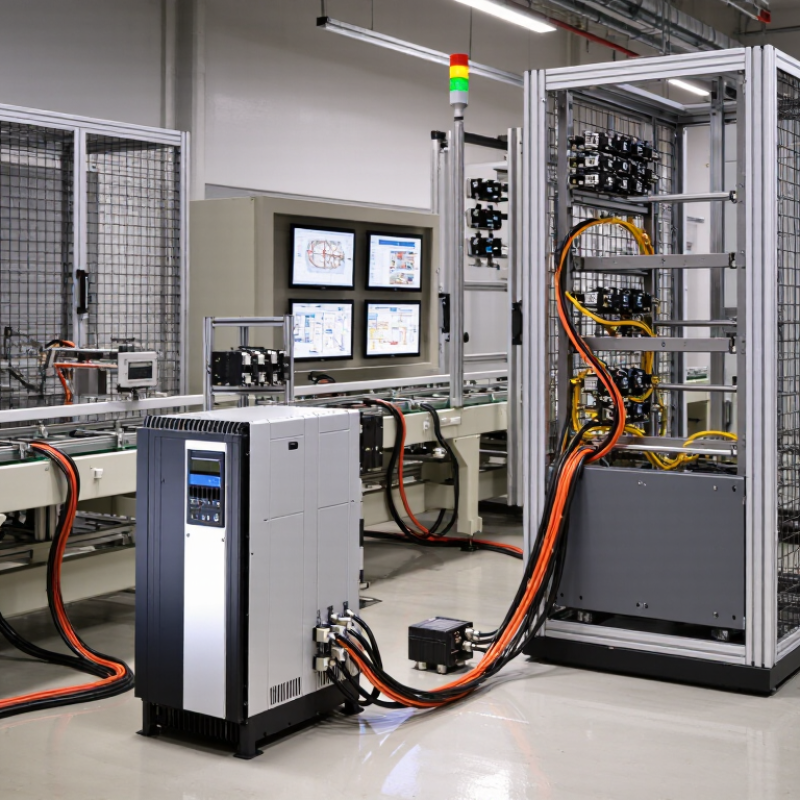
Industrial electromagnetic compatibility (EMC) means equipment can operate as intended without creating disruptive interference or failing when exposed to it. On a factory floor, a variable-speed drive may share a cable tray with sensor wiring. A poorly routed cable can turn a small electrical disturbance into a missed reading, a nuisance alarm, or an unexpected stop. EMC is therefore not just shielding. It combines equipment selection, grounding, cable routing, filtering, and testing against relevant IEC 61000 requirements.
The operational stakes are substantial, though downtime has many causes beyond EMC. Uptime Institute’s 2024 Annual Outage Analysis reported that
54% of respondents’ most recent significant outages cost more than $100,000; 16% exceeded $1 million.
These figures do not attribute outages to electromagnetic interference, but they show why preventing avoidable disruptions matters. Good EMC practice starts with the actual site: inspect noisy drives, long sensor runs, cabinet bonding, and cable separation. A design that works on a test bench may behave differently beside a welding cell. That gap deserves attention.
Tips: Keep power and signal cables apart, bond cabinet doors and panels, and document filter locations. Test during commissioning with machinery running—not only in a quiet lab. Record odd alarms, too. They may reveal a pattern, but not every fault is an EMC problem.
Industrial electromagnetic interference often begins with ordinary equipment. A variable-frequency drive can send fast voltage edges along motor cables, while relay coils create brief spikes when they switch off. Switching power supplies may add noise to shared power lines. The pattern matters.
Radiated interference can travel from poorly routed cables or large motor leads into nearby sensor wiring. A pressure reading that jumps only when a conveyor starts is a useful clue. Conducted noise may appear on power or signal lines, sometimes affecting several devices at once. Wireless transmitters and handheld radios can also disrupt sensitive receivers when placed close to control cabinets. Distance helps, but it is not a diagnosis.
Start by recording when the fault occurs: machine state, motor speed, nearby equipment, and affected signals. Then isolate likely sources one at a time, without changing several variables together. A spectrum analyzer or current probe can reveal patterns that a basic voltage check misses. Still, measurements can be misleading if the probe setup is poor. Keep cable routes, bonding points, and cabinet doors consistent during tests; small changes can shift the results. The first suspect is not always the source.
Industrial EMC solutions work best when matched to the interference path. A shielded enclosure can reduce radiated emissions from a control cabinet, especially when seams and cable entries are treated carefully. It is less effective when poor bonding leaves gaps around doors or panels. Fit matters.
For conducted noise, input filters can help keep switching interference from reaching nearby equipment. They need correct placement, short connections, and a clear grounding plan. Shielded cables are useful around variable-speed drives and sensors, but termination quality matters more than the shield alone. A loose drain connection can undo the benefit.
The application changes the choice. A compact packaging line may need cable routing changes and local filtering before a new enclosure. A dusty outdoor pump station may need robust cabinet shielding, sealed entries, and protection against transient disturbances. Test under realistic operating conditions. Motors, long cable runs, and changing loads can reveal problems that a quiet bench test misses. There is no single best package for every plant, and even a sensible design may need revision after installation. That part is easy to underestimate.
Typical application fit is shown on a qualitative 1–5 scale, not as measured attenuation or compliance-test data. Filters are commonly used to address conducted noise; shielding and cable practices help control radiated coupling; ferrites can suppress selected cable-borne interference. The best solution depends on the disturbance, frequency range, installation, and applicable EMC requirements.
In 2026, the best industrial EMC solution is the one that protects equipment without paying for unnecessary margin. Compare performance under real operating conditions: variable-speed drives, long sensor cables, and metal enclosures can create very different interference paths. IEC 61000-4-3:2020 describes radiated RF immunity testing from 80 MHz to 6 GHz. Use that test range as a reference, then check whether your site’s actual frequencies and exposure levels require additional testing. Standards set a baseline, not a guarantee.
Compliance affects cost. A shielded cabinet may reduce radiated emissions, but poor cable entry design can undermine the result. Ferrites or filters may be cheaper, yet they can add heat, space, and maintenance needs. Compare supplier quotes against test time, redesign risk, and production downtime. The European Commission’s 2023 Safety Gate report recorded 3,412 product alerts across consumer categories; it is not an EMC failure count, but it underscores why documented conformity matters. Verify each claim against the applicable product standard and a test report.
Tips: Test a representative unit before final enclosure tooling. Keep cable lengths and grounding points consistent. Small setup changes can shift results. Cost estimates should include retesting; that part is easy to underestimate.
Choosing the best industrial EMC solution for 2026 starts with the equipment’s real operating environment. A production line with variable-speed drives, long sensor cables, and frequent motor starts needs a different plan from a compact control cabinet. Record cable routes, enclosure openings, grounding points, and nearby interference sources before selecting filters or shielding. Small details matter.
Assess both emissions and immunity. A system may pass a bench test yet suffer resets when a nearby contactor switches. Test representative operating modes, including startup, peak load, and communication activity. Check cable entry points and bonding continuity; a loose panel connection can undermine an otherwise careful design. Measure, then adjust.
Choose components to address observed problems, not just to fill a specification sheet. Filters, shielded cables, and improved bonding can help, but each may affect heat, space, cost, or maintenance access. Requirements also vary by equipment type and destination, so confirm applicable standards with qualified EMC engineers and accredited testing facilities. There is no perfect shortcut. Even a well-tested installation can behave differently after a layout change, so leave room for inspection and retesting.
TERMS OF USE - LEDOLUX
This site uses cookies in order to deliver services in accordance with Privacy Policy. You can use settings within your browser to control the cookies that are set on your computer – conditions of access or storage of cookies.
Your data controller will be LEDOLUX POLAND SP. ul. Innowacyjna 1; 36-060 Głogów Małopolski, which adapts the content of its website to your needs and analyses and examines them to improve it. More information.