Choosing a Threaded Shaft End is not a minor drafting decision. It affects assembly speed, load transfer, service life, and maintenance access. A shaft may use a male thread, female thread, reduced thread, shouldered end, or double-ended design. Each option creates different stresses around the transition area.
John H. Bickford, a recognized fastener engineering authority, wrote, “The purpose of a bolted joint is to clamp two or more parts together.” That principle also guides Threaded Shaft End selection. The thread must create dependable engagement without weakening the shaft beneath it. A shoulder can position a bearing accurately. A chamfer can guide installation. A drilled end can accept a retaining screw, while a left-hand thread can resist loosening in rotating assemblies.
Small details matter. Picture a threaded shaft entering a coupling on a production line. Damaged first threads can stop assembly immediately. A sharp thread runout can become a fatigue crack under repeated torque. These failures are not always dramatic at first. They develop quietly.
This guide compares the top Threaded Shaft End types, their practical uses, and their limitations. It considers thread size, pitch, material, surface finish, engagement length, and machining accuracy. Standards remain essential, but they do not replace application judgment. That is the uncomfortable part. A technically correct thread can still fail when installation space, vibration, corrosion, or misalignment is ignored.
The right end type is not simply the strongest-looking option. It is the one that fits the load, process, and real working conditions. Reliability starts there.
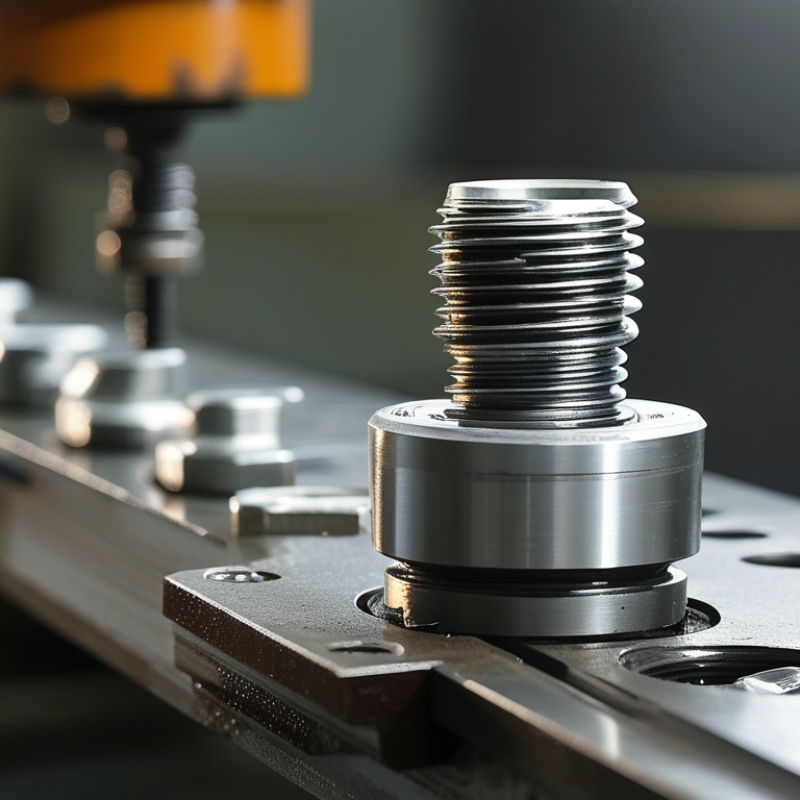
A threaded shaft end is a machined section with external or internal threads. It connects rotating parts through nuts, bolts, couplings, bearings, or adjustable collars. External male threads suit nuts and retaining rings. Internal female threads accept bolts in compact assemblies. Stepped ends add a shoulder for accurate axial positioning. Reduced threads help connect shafts with different diameters. Stud-style ends support repeated assembly and disassembly.
These details affect torque transfer, preload, alignment, and maintenance. A shaft end must resist twisting and axial movement without damaging its threads. ISO 898-1 defines mechanical property classes for fasteners, but shaft design needs separate stress calculations. Thread engagement is not a magic number. Material strength, pitch, lubrication, and loading direction all matter.
Industry data shows why small details deserve attention. The U.S. Department of Energy’s 2022 Industrial Motor Systems Market Assessment reports that motor systems use about 68% of manufacturing electricity. Many of these systems rely on rotating shafts and mechanical connections. A worn thread can create vibration, looseness, and costly downtime. The Global Wind Energy Council reported 117 GW of new wind capacity installed in 2023, highlighting the growing need for reliable rotating equipment. Still, a larger thread is not always better. I have seen designs overlook shoulder clearance, making bearing replacement unnecessarily difficult. Engineers should verify thread tolerances, runout, fatigue loads, and service access before selecting an end type.
Threaded shaft ends are classified by thread position, shaft geometry, and connection purpose. The common groups include externally threaded ends, internally threaded ends, stepped ends, shoulder ends, and reduced-diameter ends. An external thread accepts a nut or threaded coupling. An internal thread receives a screw or male stud.
Thread direction creates another useful classification. Right-hand threads dominate general machinery, while left-hand threads suit rotating assemblies that could loosen during operation. Engineers also separate full-length threads from partial threads. Partial threads leave a smooth land for bearings, seals, or axial positioning. Metric and Unified inch threads require different gauges, pitches, and tolerance checks. ISO 261 covers preferred metric thread sizes, while ASME B1.1 defines Unified thread forms.
Geometry affects load transfer. A shoulder end can locate a component against a fixed face. A reduced end lowers clearance and may protect a larger shaft section. A stud-style end supports repeated assembly without damaging the main shaft.
Fit matters. According to Grand View Research, the global industrial fasteners market reached approximately 86.1 billion dollars in 2023, reflecting strong demand across machinery and maintenance applications. However, that figure covers many fastener categories, not threaded shaft ends alone. This limitation deserves attention.
In practice, technicians inspect thread crest damage, runout, pitch, and shoulder squareness. A caliper helps, but it cannot confirm thread class. Thread gauges provide better control. Measure twice. A clean drawing should state thread standard, diameter, pitch, length, hand, and tolerance. Missing one detail can produce an apparently correct part that fails during installation.
Threaded shaft ends connect gears, couplings, bearings, and adjustable mechanisms. The main designs include external threads, internal tapped holes, stepped threads, and double-ended threads.
External threads suit nuts and retaining collars. Internal threads save space inside compact assemblies. Stepped ends combine a bearing seat with a smaller threaded section. Double-ended designs support two separate components, but alignment becomes more demanding.
Thread form matters as much as shaft shape. Metric threads offer broad international compatibility. Fine threads provide better adjustment and stronger clamping under the same diameter. Coarse threads assemble faster and resist damage in dirty environments. Left-hand threads can prevent loosening during rotation, although they may confuse maintenance teams.
MarketsandMarkets’ 2024 linear motion market report projects continued growth through 2029, driven partly by automation and precision equipment. That trend increases demand for repeatable shaft geometry, but market forecasts cannot replace torque testing. A clean drawing can still hide a weak shoulder.
Tips:
Match thread diameter, pitch, engagement length, and load direction before ordering. Keep the first thread away from sharp shoulders. Add a small relief groove when the shaft requires full seating.
Check runout after machining, not only thread dimensions. ISO 898-1 material classes help evaluate fastener strength, yet the shaft material and actual loading remain critical.
In practical inspection, burrs near the thread start often cause more trouble than expected. This detail is easy to overlook.
What Are the Top Threaded Shaft End Types?
Selecting the right threaded shaft end begins with the load, not the thread alone. Male-threaded ends suit direct attachment to nuts, couplers, and adjustable supports. Female-threaded ends protect the shaft profile and accept bolts or threaded rods. Stud ends work well where repeated assembly is expected. A shoulder can also locate a bearing or spacer accurately.
Measure carefully. Thread diameter, pitch, engagement length, and end geometry must match the mating component. A fine thread may provide precise adjustment, while a coarse thread handles dirt and faster installation more effectively. Check the axial load, bending force, rotation speed, and tightening torque. Small errors matter.
The shaft material and environment deserve equal attention. Stainless or coated steel may resist moisture, but coating thickness can alter thread fit. In abrasive areas, exposed threads need protection during handling. Avoid selecting a threaded end from a catalog image alone. A drawing can look complete yet omit the required shoulder length. That happens more often than expected. Verify the mating part with a thread gauge, caliper, and sample assembly. Leave enough engagement to carry the load, but not so much that the shaft bottoms out. If rotation reverses, inspect the thread direction carefully. A right-hand thread may loosen in service. Test the connection under realistic movement before approving production.
Threaded shaft ends usually fall into five practical types: male studs, female threaded bores, reduced threaded ends, shoulder ends, and stepped ends. Each design creates different machining and inspection risks. Male threads suit direct fastening. Female bores protect external surfaces and reduce snagging. Shoulder ends provide a clear seating surface, but shoulder squareness becomes critical.
Turning, thread rolling, or thread cutting can produce these profiles. Thread rolling often improves surface strength, while cutting offers greater flexibility for small batches. ASME B1.1 defines Unified thread profiles, and ISO 965-1 specifies metric thread tolerance principles. These standards help engineers control pitch diameter, flank angle, and fit. A clean thread crest is not enough. Burrs at the runout can prevent full engagement.
Inspection should combine visual checks, calibrated GO/NO-GO gauges, and dimensional measurement. ISO 14253-1 emphasizes measurement uncertainty when accepting or rejecting parts. NIST’s Engineering Statistics Handbook also separates repeatability from reproducibility, which matters when several inspectors use the same gauge. Check runout near the shoulder. Measure thread length. Verify concentricity against the shaft datum. A perfect gauge result can still hide a bent end or poor shoulder contact.
Tips: Specify the thread standard, tolerance class, usable thread length, and runout limit on the drawing. Inspect the first article after tool changes. Keep gauge records. Review rejected parts honestly; some failures come from unclear drawings, not poor machining.
TERMS OF USE - LEDOLUX
This site uses cookies in order to deliver services in accordance with Privacy Policy. You can use settings within your browser to control the cookies that are set on your computer – conditions of access or storage of cookies.
Your data controller will be LEDOLUX POLAND SP. ul. Innowacyjna 1; 36-060 Głogów Małopolski, which adapts the content of its website to your needs and analyses and examines them to improve it. More information.